The following procedure is the upgrade that needs to be implemented in order to fix
attachment problems with plates. (See the attached pictures).
There is a another symptom that is caused by attachments with lines on the plate.
The Modification is not mandatory if you are not experiencing problems with
attachments.
We strongly recommend performing the entire modification as described in this
procedure.
Attachments Samples showing on plates
Figure 1. Problem #1
Figure 2. Problem #2
After several tests in the production line, the following are recommended procedures
for solving the problem.
Please read these instructions thoroughly before beginning to
drill the drum.
Dismount the unloading tray.
Polish the drum with a polish stone, at the zones where there are plate attachment
problems.
Clean the drum with alcohol.
Lock the drum in the best position for drilling.
Use a vacuum cleaner during drilling the holes.
Use the air drill from the Kit (High-speed drill).
Execute the following steps to drill holes in the drum:
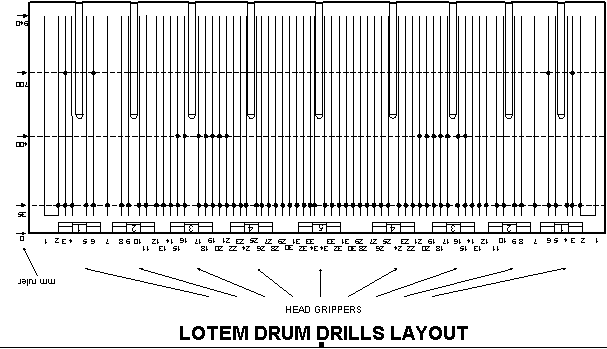
Draw a line with a pencil across the drum in position 400 mm and 700 mm.
Drill and widen with 1.6 mm diameter drill bit the first row of existing holes (at row
35 mm),
Drill new holes (at row 400 mm) with 1.6 mm diameter drill bit in the
vacuum grooves at numbers 15 to 21 on each side of the drum (total of fourteen holes to be
drilled).
Drill new holes (row 700 mm) with 1.6 mm diameter in vacuum grooves
numbers 3 and 6 on each side of the drum (total of four holes drilled).
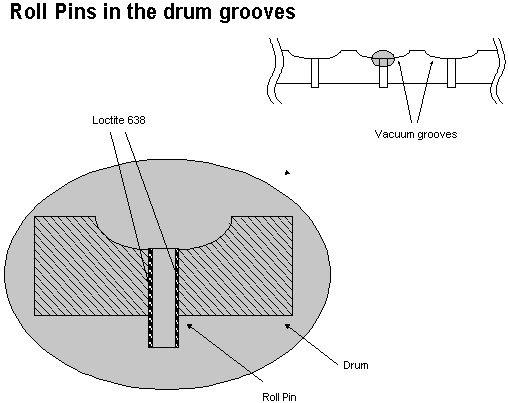
Use the enclosed tool to insert the special roll pins from the kit with Locktite 638
into the newly drilled holes.
Clean the excess Locktite from the drum and clean also inside the roll pins with a
0.9-mm drill bit.
Tools Kit:
Polish stone 1
Air driller 1
Roll pin tool 1
Drill soap. 1
Parts 10
Parts:
Drill bit 1.6 mm 5
Drill bit 0.9 3
Locktite 638 1
Roll pin 90 (six spears).
Follow the attached drawings when implementing the modification.